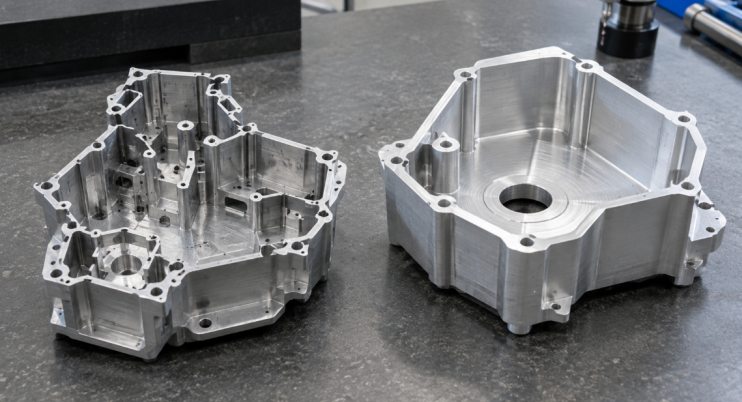
A CNC machining service turns your 3D model into precise metal or plastic parts by milling away material. The right factory gives you tight tolerance, the right material, and a clean path from first prototype to full production. Goldconn runs this as a core process on its CNC machining and turning line.
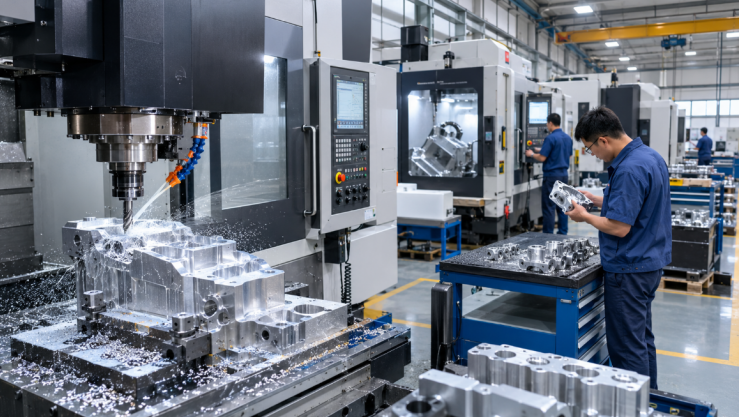
Table of contents
- 1. What a CNC Service Should Provide
- 2. Machine Fleet and Axis Capability
- 3. Material Machinability Across Alloys
- 4. Tolerance, GD&T, and How to Specify Them
- 5. Surface Finish and Post-Processing
- 6. Prototyping Speed and First Articles
- 7. Scaling from Prototype to Production
- 8. Quality Control and Traceability
- 9. Communication and DFM Collaboration
- 10. Questions to Ask Before You Commit
1. What a CNC Service Should Provide
Before you compare factorys, settle what “good” means for your program. Four pillars decide whether a CNC supplier will actually deliver: capacity to meet your volume, capability to cut your geometry, a documented tolerance it can prove, and a quality system that catches problems before parts ship. A factory strong on only one or two of these will bottleneck you later.
CNC’s biggest structural advantage is that it needs no tooling. That means low startup cost, instant design changes, and no wait for a die or press tool. For a side-by-side with another process, see CNC machining vs sheet metal fabrication.
1.1 Capacity, Capability, and Proof
Capacity is simply how many machines and shifts the factory can devote to you. Capability is the axis range and fixture know-how to cut your shape. Proof is the part you can inspect yourself: CMM reports, first-article data, and a quality certificate. Treat any one of these as missing until the supplier shows it, not just claims it.
2. Machine Fleet and Axis Capability
Axis count decides what shapes a factory can cut in one setup. Three-axis moves the tool in X, Y, and Z, which covers pockets, faces, and simple contours. Four-axis adds a rotary axis so the part can turn while milling, reaching side features without refixturing. Five-axis tilts and rotates the part so angled holes and sculpted surfaces are cut in a single hold, protecting accuracy and shrinking setup time.
2.1 What Each Axis Level Unlocks
| Axis level | What it cuts well | When you need it |
| 3-axis | Flat faces, pockets, drilled holes, simple contours | Most brackets, plates, and enclosures |
| 4-axis | Side features, circumferential holes, turned profiles | Parts with features around a rotary axis |
| 5-axis | Angled holes, sculpted surfaces, compound contours | Aerospace, medical, complex housings in one setup |
Goldconn runs 150 plus CNC machining centers across three facilities, including 3-, 4-, and 5-axis machines, so both straightforward and complex parts scale under one roof. The practical takeaway: match the axis level to your geometry, because forcing a five-axis part onto a three-axis machine multiplies setups and risk.
3. Material Machinability Across Alloys
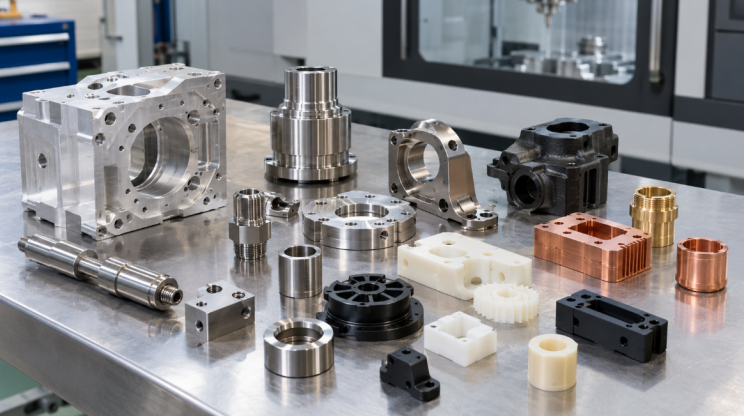
Not all metals cut the same, and the difference shows up in tool life, cycle time, and surface quality. Aluminum is easy and fast, which is why it dominates prototypes and housings. Stainless tends to work-harden, so it needs sharp tools and steady feeds to avoid glazing. Titanium is strong and heat-sensitive, so it runs slower with care to keep the cut cool. Carbon steel sits in the middle and machines predictably.
3.1 Materials Goldconn Machines
| Family | Examples | Machining note |
| Aluminum | 6061, 7075, 2024, 5052 | Fast, clean chips, ideal for prototypes |
| Stainless | 303, 304, 316, 17-4PH | Work-hardens; sharp tools, steady feed |
| Carbon steel | 1018, A36, 4140, 4340 | Predictable, good for structural parts |
| Copper and brass | Copper, brass alloys | Soft, gummy; needs correct tool geometry |
| Titanium | Grade 2, Grade 5 | Strong, heat-sensitive; slower, cooled cuts |
| Magnesium | AZ series | Light, fast; handled with care for safety |
| Tool steel | A2, D2, H13 | Hard; used for fixtures and molds |
| Engineering plastics | ABS, PC, Nylon, POM, HDPE, PEEK, PTFE, Acrylic | Each has its own feed and support needs |
A broad in-stock list matters because material availability drives both lead time and price. When casting is on the table instead, read die casting vs CNC machining to weigh the trade.
4. Tolerance, GD&T, and How to Specify Them
Tolerance is where CNC earns its keep. Goldconn holds about plus or minus 0.01 mm on key features, depending on geometry and material. The key word is “key features”: calling out that tight number on every dimension wastes money, so specify it only where function demands it.
4.1 Reading Your GD&T
For parts with datums and true-position calls, the factory should read your GD&T and hold the relation between features, not just each size in isolation. A hole pattern located to a datum can be held as a group even if the absolute position drifts slightly, which is usually what the assembly actually needs. Tie dimensions to a common datum wherever you can.
| Specifying approach | Result | When to use |
| Tight call on every dimension | Higher cost, slower cut, more inspection | Rarely; only true precision needs |
| Tight call on key features only | Best cost-accuracy balance | Most production parts |
| GD&T with datums | Function-based control, less over-spec | Assemblies and located features |
5. Surface Finish and Post-Processing
Machined parts leave the spindle with tool marks; the finish you need decides extra steps. A cosmetic housing may want bead blast or brushed look, while a wear surface may need a harder coating. Secondary work such as tapping, threading, and deburring often follows the cut.
| Finish or process | What it does | Typical use |
| Bead blast | Uniform matte texture | Housings, consumer-facing parts |
| Anodize | Hard, corrosion-resistant oxide layer | Aluminum structural and visual parts |
| Passivation | Restores stainless corrosion resistance | Medical and food-adjacent parts |
| Plating | Conductive or wear surface | Contacts, bushings |
| Polishing | Smooth, reflective surface | Seals, optics mounts |
Ask the factory which finishes it runs in-house so you avoid handing the part to a second vendor, which adds lead time and a hand-off risk. Goldconn lists common finishes and can advise on sourcing the rest.
6. Prototyping Speed and First Articles
Because CNC needs no tooling, the first article is limited mainly by part complexity and machine queue, not by a tooling build. That makes CNC the fastest route from a finished model to a real metal part you can test. You can also revise the model and cut the next one without re-tooling, which is why engineering teams use CNC through the whole validation phase.
Use the prototype to confirm fit, function, and thermal behavior before committing to volume. A part that validates on a CNC prototype carries far less risk into production than one that was only simulated.
7. Scaling from Prototype to Production
CNC shines when volume changes. With no tooling, moving from ten parts to ten thousand is a matter of machine time and scheduling, not a new investment. Goldconn supports fast first articles and scales to volume across its 58,000 m2 of manufacturing space and 800 plus staff, with processes certified to ISO 9001, ISO 14001, ISO 45001, QC 080000, and IATF 16949. This is part of the broader custom metal fabrication services program.
One caution: at very high volume, casting or stamping may beat CNC on unit cost because their tooling spreads across many parts. The right process can shift as your annual volume rises, which is why the DFM review looks at both your prototype and production scale.
8. Quality Control and Traceability
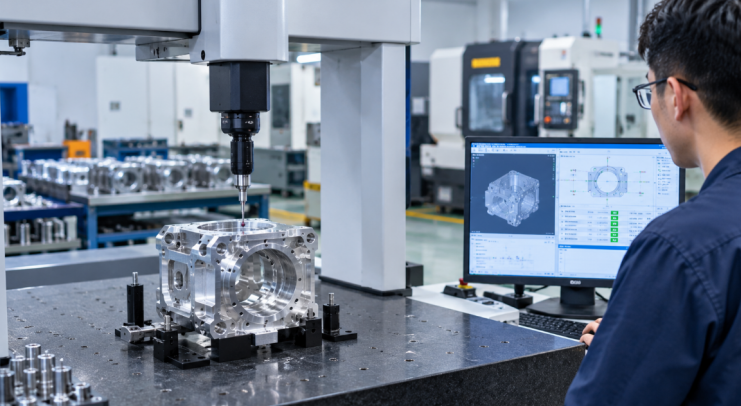
Parts are checked on CMM to confirm size and geometry, with first-article inspection and in-process checks as volume grows. For automotive and medical, the certified system and per-batch traceability matter as much as the measured number. Goldconn keeps full material and process records so a part can be traced back through its run, and incoming alloy is verified before production.
Ask how the factory proves a tolerance, not just what it claims. A CMM report tied to your drawing, plus material certification, is the evidence that protects your schedule and warranty.
9. Communication and DFM Collaboration
The cheapest improvements usually come from a DFM conversation before you cut metal. A good supplier flags features that raise cost or risk and proposes a cheaper capable path while the design is still flexible. Goldconn runs this review free and returns it with a quote within 24 hours, so you get expert feedback without committing to a build.
Communication also covers responsiveness during production: lead-time updates, change control, and a clear person to call. These soft factors decide whether a supplier stays a partner or becomes a fire to manage.
10. Questions to Ask Before You Commit
| Question | Why it matters | Red flag |
| What axis range do you run? | Decides geometry it can cut in one setup | Only 3-axis for a complex part |
| What tolerance can you hold and prove? | Separates claim from CMM evidence | No inspection report offered |
| Which materials do you stock? | Affects lead time and price | Must source your alloy externally |
| How do you inspect? | Shows quality maturity | Visual only, no CMM |
| Can you scale to my volume? | Protects production ramp | Unclear capacity plan |
See the full scope on the metal manufacturing services page. A clear answer on all five tells you whether the factory fits prototype-to-production work.
Frequently Asked Questions
- Is CNC good for low volume? Yes. With no tooling, CNC is ideal for prototypes and small runs, and easy to revise.
- What tolerance can CNC hold? Goldconn holds about plus or minus 0.01 mm on key features, depending on geometry and material.
- Which materials can be machined? Aluminum, stainless, carbon steel, copper, brass, titanium, magnesium, tool steel, and many engineering plastics.
- How fast is the first article? CNC needs no tooling, so first articles are fast; exact timing depends on part complexity and queue.
- Does five-axis matter for my part? If your part has angled holes or contoured faces, five-axis cuts them in one setup, protecting accuracy.
- Can you anodize or plate in-house? Ask which finishes the factory runs directly; Goldconn lists common ones and can advise on sourcing.
- How do you prove tolerance? On CMM, with first-article and in-process checks as volume grows.
- Will CNC stay cheaper at high volume? Not always. Casting or stamping can beat CNC per part at high volume; the DFM review compares both.
- Can you machine plastics too? Yes. ABS, PC, Nylon, POM, HDPE, PEEK, PTFE, and Acrylic are all on the list.
- How do I get a quote? Send your model and volume. Goldconn returns a free DFM review and a quote within 24 hours.
Request a Free DFM Review
Looking for a CNC partner from prototype to production? Send Goldconn your model and volume. You get a free DFM review and a quote within 24 hours, with 3-, 4-, and 5-axis capacity under one roof.